Paper Bag Making Machine Service Guide for Optimal Performance
2026-11-02
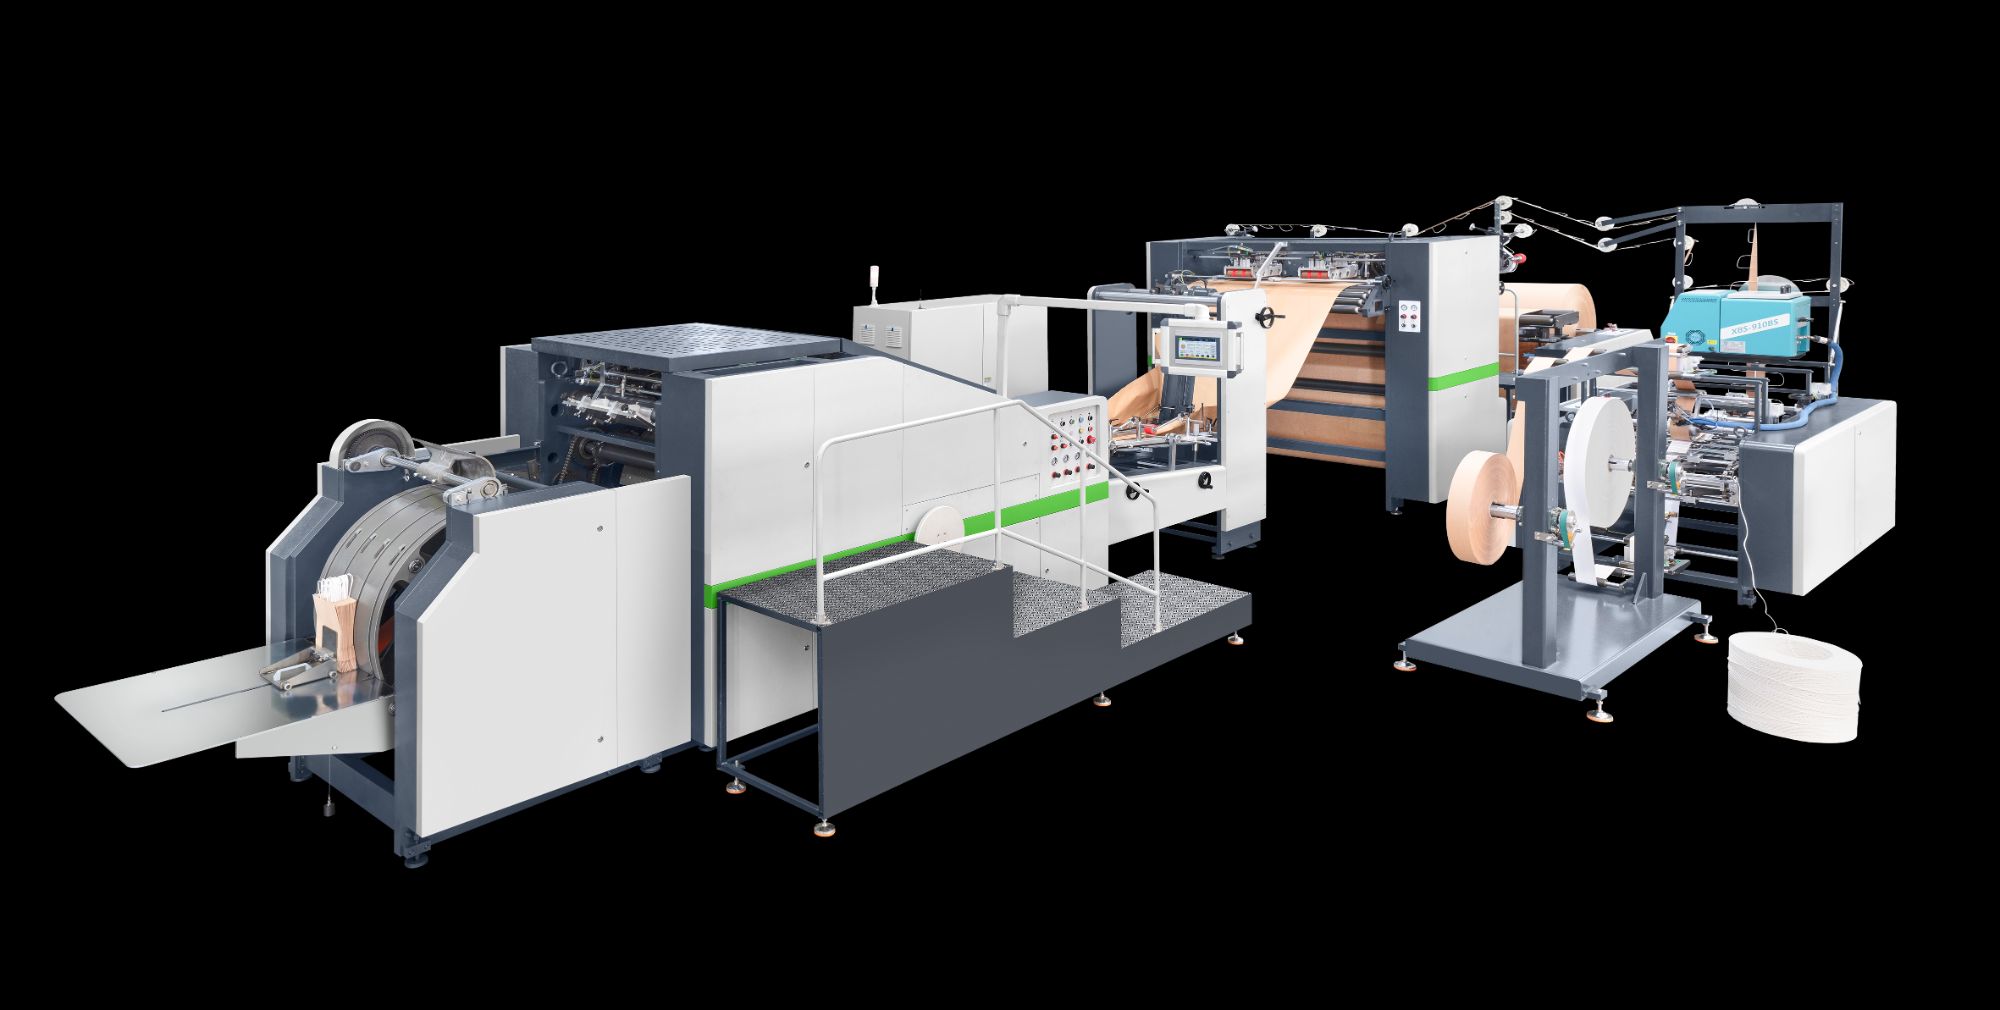
Paper bag making machines rarely stop without warning—they lose precision first. Seals weaken, tension drifts, and waste climbs before anyone notices. That’s why a service guide built for optimal performance matters more than a generic maintenance checklist. Here, we look at the routines that keep bag quality consistent and unplanned downtime rare. With ROKIN machines, we’ve seen how small, consistent checks—rollers, sealing bars, lubrication—prevent the failures that eat into margins. Follow along to see which habits actually move the needle.
The Paper Bag Machine Bearing Failure That Starts with a Faint Whine
It begins as the kind of faint whine that gets written off as a speed change or a dull blade somewhere down the line. On a paper bag machine, that thin metallic edge usually points to a bearing starting to run dry, with the lubricant film no longer keeping rollers and raceways apart. A quick infrared reading and a close look at the grease around the housing can confirm whether the sound is coming from a failing bearing before it turns into a shutdown.
Once the whine thickens into a low growl, the damage has already moved beyond surface polish. The raceway starts spalling, metal dust circulates through the remaining grease, and the extra drag shows up as uneven fold lines or a slight drift in seal placement. Rather than waiting for the bearing to seize and snap a shaft or chew up a coupling, the line should be stopped for a targeted replacement—downtime at that point is measured in minutes, not the hours a catastrophic failure would cost.
Why a Resharpening Schedule Beats a Replacement Budget for Your Cutting Station
Most shops treat saw blades and router bits as consumables with a rough replacement budget, but that approach quietly drains money. A resharpening schedule flips the logic: instead of buying new tooling on a calendar, you keep a small rotation of sharpened edges ready and swap them before performance drops. The result is less variation in cut quality, fewer emergency orders, and a lower cost per linear foot over a year.
The real advantage shows up in downtime. When a blade gets dull, feed rates slow, burns appear on edges, and operators compensate with extra passes or sanding. A schedule eliminates that guessing. You pull the tool after a set number of hours or board feet, send it out, and install a fresh edge in minutes. The machine keeps running at the same speed instead of degrading until someone notices a problem.
Replacement budgets also hide the true cost of neglect. A chipped carbide tip can ruin a workpiece or stress a spindle bearing. Resharpening costs a fraction of a new blade and extends the body life several times over. Over a year, a cutting station on a resharpening schedule often spends 30 to 40 percent less on tooling than one that simply replaces blades when they fail.
Operator Habits That Extend Paper Bag Machine Life More Than Any Upgrade
Most operators ignore the slow buildup of paper dust and glue residue, but those are the real killers of precision parts. Taking ten minutes at the end of each shift to vacuum the roller housings, wipe down the folding plates, and clear the cutter area does more than any retrofit. A quick finger-press check on belt tension while the machine is still warm catches slack before it becomes a tracking problem.
Lubrication is not a case of more is better. Knowing exactly which bearings need a light touch of food-grade grease and which pivot points must stay dry prevents the kind of premature wear that upgrades can’t reverse. Experienced operators learn to listen for a dry squeak or a slight rattle at specific speeds, then address only that spot instead of greasing everything on a fixed schedule. A small handwritten log of odd noises, temperature changes, or a misaligned fold line helps catch trouble while it is still cheap to fix.
The habits around startup and shutdown matter just as much as mid-run adjustments. A slow-speed test run before full production lets you feel a rough spot in the feed mechanism or see a weak seal before it turns into a jam. Letting the machine clear its paper path at the end of the day keeps hardened adhesive from setting on the forming shoulder. None of this costs money, but it consistently beats any upgrade because it targets the small, daily wear that upgrades never address.
Electrical Faults That Mimic Mechanical Jams and How to Tell Them Apart
A photocopier that refuses to feed paper might look like a classic roller jam, but a failing clutch or a worn drive gear can produce the same hesitation without any torn sheets in the path. One reliable clue is sound: mechanical jams usually create a rhythmic grinding or thumping as rollers slip on stuck media, while electrical faults often cause abrupt stops with a faint click from a relay or no noise at all. If you clear an empty paper path and the machine still stalls at the same point in the cycle, suspect a sensor or motor driver rather than paper debris.
Voltage drops to a feed solenoid can mimic the resistance of a crumpled page, especially when the fault is intermittent. Watch for patterns that don't match physical obstructions—like jams that occur only after the machine warms up, or that vanish when you reseat a connector. A quick test: manually rotate the feed rollers with the power off. If they move freely and evenly, the problem is likely in the control board, wiring harness, or a failing power supply, not in the mechanical drive train.
Another giveaway is the error history. Electrical faults tend to scatter across different jam codes or throw generic motor errors, while a true mechanical jam usually repeats the same sensor location every time. Swap a known-good paper tray or cassette if possible; a marginal tray sensor can send a "paper present" signal that drops out mid-feed, mimicking a crumpled leading edge. Before replacing gears or rollers, check for bent connector pins, cracked solder joints on the driver board, or a weak solenoid that doesn't fully retract the pickup arm—these electrical culprits often masquerade as stubborn mechanical failures.
What Should a Weekly Inspection Cover on a Paper Bag Machine?
A weekly inspection should start with the areas that wear down fastest under daily use. Check the feed rollers for uneven wear or paper dust buildup, which can cause misfeeds or bag length drift. Inspect the glue application system—nozzles, hoses, and reservoirs—for dried adhesive or partial clogs, as these lead to weak seams or messy overlaps. Don't overlook the cutting blades: even a slight dullness changes bag dimensions and leaves ragged edges, so feel the blade edges and verify the cut quality against the last production sample.
Next, turn your attention to the moving parts that take the most punishment. Look closely at the chain and belt tensions, especially the main drive and the delivery conveyor, because a loose belt often mimics an electrical fault. Give the bearings on the gusset folder and bottom former a quick temperature check with the back of your hand—any spot that feels noticeably warmer than the surrounding frame deserves a closer look. Listen for irregular sounds while the machine runs at low speed: a faint clicking from the cam followers or a slight knock near the connecting rods can point to a developing issue long before it stops production.
Finally, make the inspection actionable rather than just a visual pass. Record the gap measurements on the folding plates and compare them with the baseline from the previous week; a drift of even a couple millimeters changes the bag's squareness. Clear out the scrap collection area and note the pattern of discarded bags—an increase in one corner tear usually indicates a specific station needs adjustment. If your machine has a perforation unit, test the tear-off line on a few bags by hand instead of relying on the counter's count, since static or blade residue can fool the sensor. Wrap up by verifying that all emergency stop buttons and guard interlocks respond correctly; a weekly check that skips safety hardware isn't really a check at all.
Tension Settings That Stop Crushing Paper and Slash Film Waste
Dialing back tension isn't a one-size-fits-all move. For corrugated and lightweight paperboard, start at the lowest workable setting and nudge up only until the load stops shifting on a test run. Too much force bows side panels and tears roll ends before you see it on camera, but the damage shows up downstream as rejected pallets.
Pre-stretch makes a bigger difference than most operators assume. If the film is stretched at the carriage before it hits the load, you can drop overall wrap force dramatically and still get tight, stable containment. That cuts film use per pallet because you're not relying on extra revolutions to compensate for slack. The waste reduction comes from eliminating snapped film tails, loose corners, and double-wrap habits.
Set tension by load profile, not by habit. Palletized paper bags, tissue bundles, and chipboard cartons each need different force curves. A good rule is to run the lowest containment force on the lightest face, then program one extra layer only on the corners or top band where movement actually occurs. Operators who log those settings by SKU stop reinventing the setting every shift, and the film waste drops fast.
FAQ
Wipe down the feed rollers and forming plates at the end of each shift, then use compressed air to clear dust from the sensor housings. Weekly, inspect the chain tension and apply a thin coat of food-grade grease to the cam followers, but avoid over-lubricating the guide rails as that attracts fiber buildup.
Rubber feed rollers need a dry silicone spray every 40 operating hours, while the gearbox oil should be replaced after the first 500 hours and then every 2,000 hours. The rotary scoring bearings work best with a light lithium grease every two weeks, but always wipe off excess to prevent paper dust from sticking.
You will notice ragged edges on the bag mouth or a dull thud instead of a clean snap during cutting. If the blade leaves faint tear marks on the paper surface or requires noticeably more force to complete the stroke, it has likely lost its edge. Replace it immediately once you see micro-chipping along the bevel.
Misaligned folds often trace back to uneven wear on the folding plates or a slight drift in the side-lay guide. Check whether the paper roll tension is consistent from left to right, then verify that the folding fingers are not bent by a previous jam. A quick test: run five bags and measure the distance from the fold line to the edge; if it varies more than 0.5 mm, recalibrate the side guide.
Keep the paper path free of static by installing an anti-static bar near the unwind stand, and ensure the brake tension drops smoothly rather than pulsing. Pre-fold the leading edge of a new roll before splicing, and run the machine at half speed for the first 200 bags after a roll change. Also, vacuum the perforation wheel every two hours to stop paper chads from lodging in the teeth.
Set the glue wheel to contact the paper at a 15-degree angle, and maintain a constant adhesive temperature within plus or minus 3 degrees Celsius. Use a viscosity cup check every morning; if the glue thickens, add the manufacturer's recommended thinner in small increments while the machine is running. Clean the glue nozzles with warm water after each batch and replace the doctor blade if you see streaking.
Recalibrate whenever you change paper grammage or bag size, and also if you notice the bag length drifting by more than 2 mm across a run. Perform a two-point calibration using a known short bag and a long bag, then run ten consecutive bags at normal speed and compare the cut positions against a reference mark.
Conclusion
A paper bag making machine rarely fails without warning, but the earliest signs are easy to miss. A faint whine from a bearing might seem harmless until heat and wear turn it into a seized roller. Catching that sound during routine operation can save days of downtime. Similarly, the cutting station doesn't always need new blades; a disciplined resharpening schedule keeps edges precise and avoids the hidden cost of frequent replacements. Operator habits play an even bigger role than hardware upgrades—simple routines like keeping feed paths clean and not forcing misaligned stock prevent most unexpected stops.
Electrical issues often masquerade as mechanical jams. A motor that stutters or a sensor that drops signal can mimic a paper blockage, so check voltage and connections before tearing into the drive train. A weekly inspection should cover bearing temperatures, cutting edge condition, belt tension, and control panel error logs, not just visual cleanliness. Finally, tension settings are the silent killer of quality: too tight crushes the paper and jams the forming plates, while too loose leads to film waste and sloppy seals. Steady, measured adjustments—not guesswork—keep the line running smoothly and extend service life far beyond what any single upgrade could achieve.
Contact Us
Contact Person: CARA
Email: [email protected]
Tel/WhatsApp: +8619519778302
Website: https://www.rokinmachinery.com